2026-02-09•5 min cable extrusion•VIESUNCO Materials Science Team

Halogen-Free Flame Retardant Cable Extrusion: Preventing Screw Scorching & Passing UL94 V-0

Flame retardant fillers can cause screw build-up and rough surface texture. Practical tips on screw L/D ratio, screen mesh selection, and temperature profiles.

#Cable Extrusion#Halogen-Free#Screw Tuning#UL94 V-0#Extrusion Tips
Halogen-Free Flame Retardant Cable Extrusion: Preventing Screw Scorching & Passing UL94 V-0

1. Extrusion Temperature & Screw Setup

Halogen-free metal hydrate flame retardants decompose if shear heating is excessive:
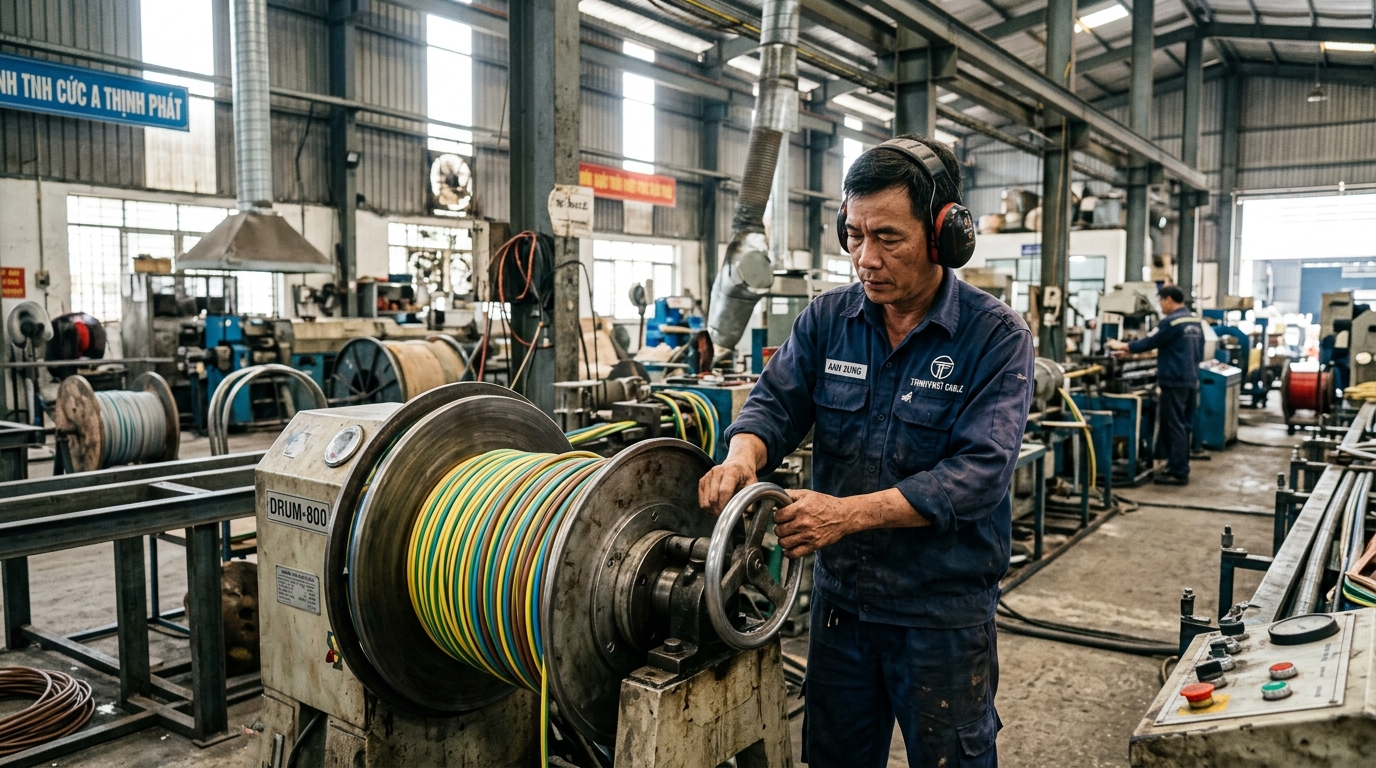
Industrial Wire and Cable Extrusion Reeling Machine
▲ Industrial Wire and Cable Extrusion Reeling Machine
  • Gradual Barrel Heat: 140°C feed, 160°C compression, 170°C metering, 175°C die. Keep below 190°C.
  • Screen Mesh: Use 40/80/40 mesh pack to balance filtration and backpressure.
  • Purging: Always purge with raw PP or clear TPE for 10 minutes before daily shutdown.

Need a Custom TPE/TPR Formulation for Your Application?

Our polymer engineering team provides 1-on-1 technical consulting, tooling support, and complimentary testing samples.