1. Why TPE Flashes Easily
TPE is a shear-thinning polymer with low melt viscosity under high pressure:
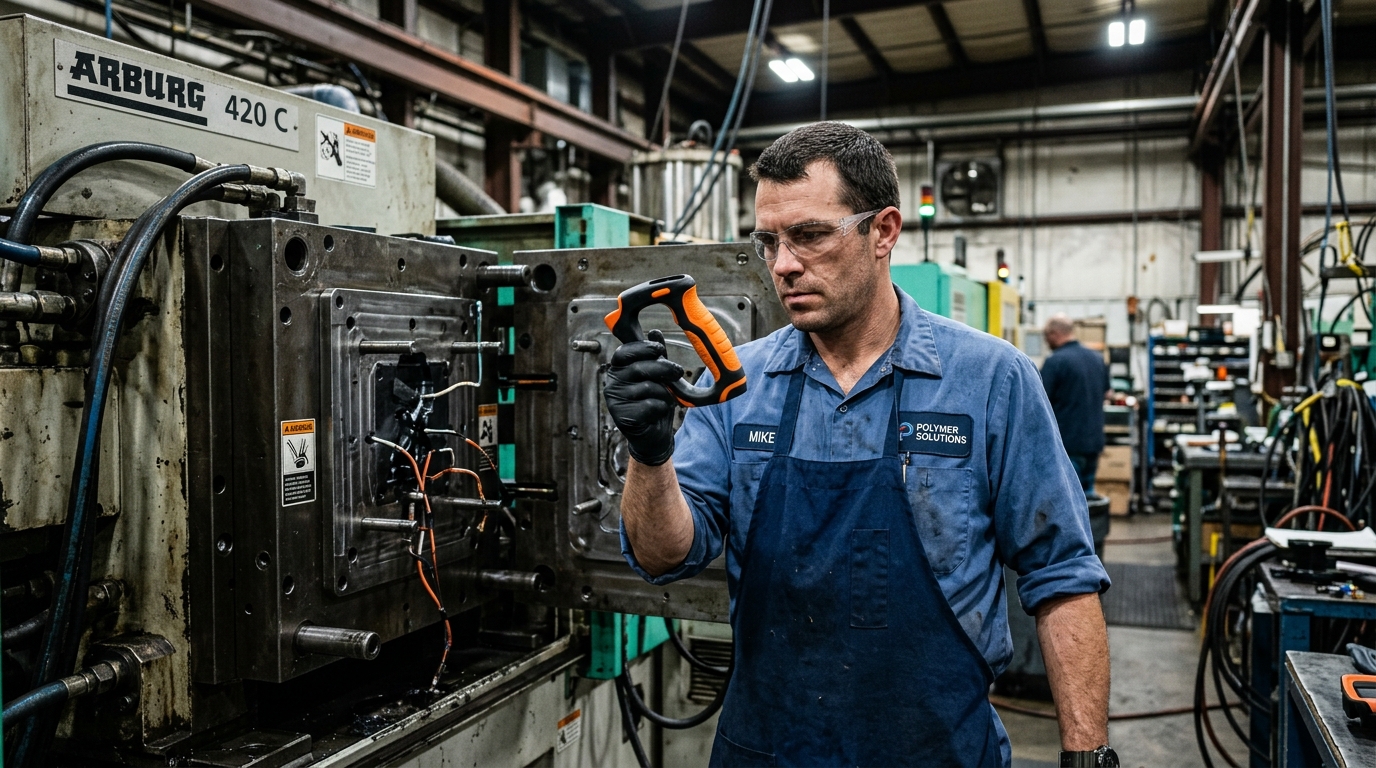
- Vent Depth: Venting slots must be machined between 0.012mm and 0.018mm.
- V/P Switchover: Switch to holding pressure when cavity is 95%–98% filled.
Manual trimming of flash eats your profits. Learn optimal cavity vent depth (0.015mm), V/P switchover points, and barrel shear management to eliminate flash and peeling.
TPE is a shear-thinning polymer with low melt viscosity under high pressure:
Our polymer engineering team provides 1-on-1 technical consulting, tooling support, and complimentary testing samples.
Footwear soles or tool handles: should you pick TPE or TPR? A practical comparison on wear, thermal resistance, regrind ratios, and tuning tips for mold shrinkage.
2026-02-10A realistic cost-benefit breakdown for footwear & electronics OEMs in Vietnam: freight fees, customs delays, fast sampling, and working capital savings.