1. Top 3 Causes of Overmolding Peeling
Simply raising injection temperature does not fix bonding issues:
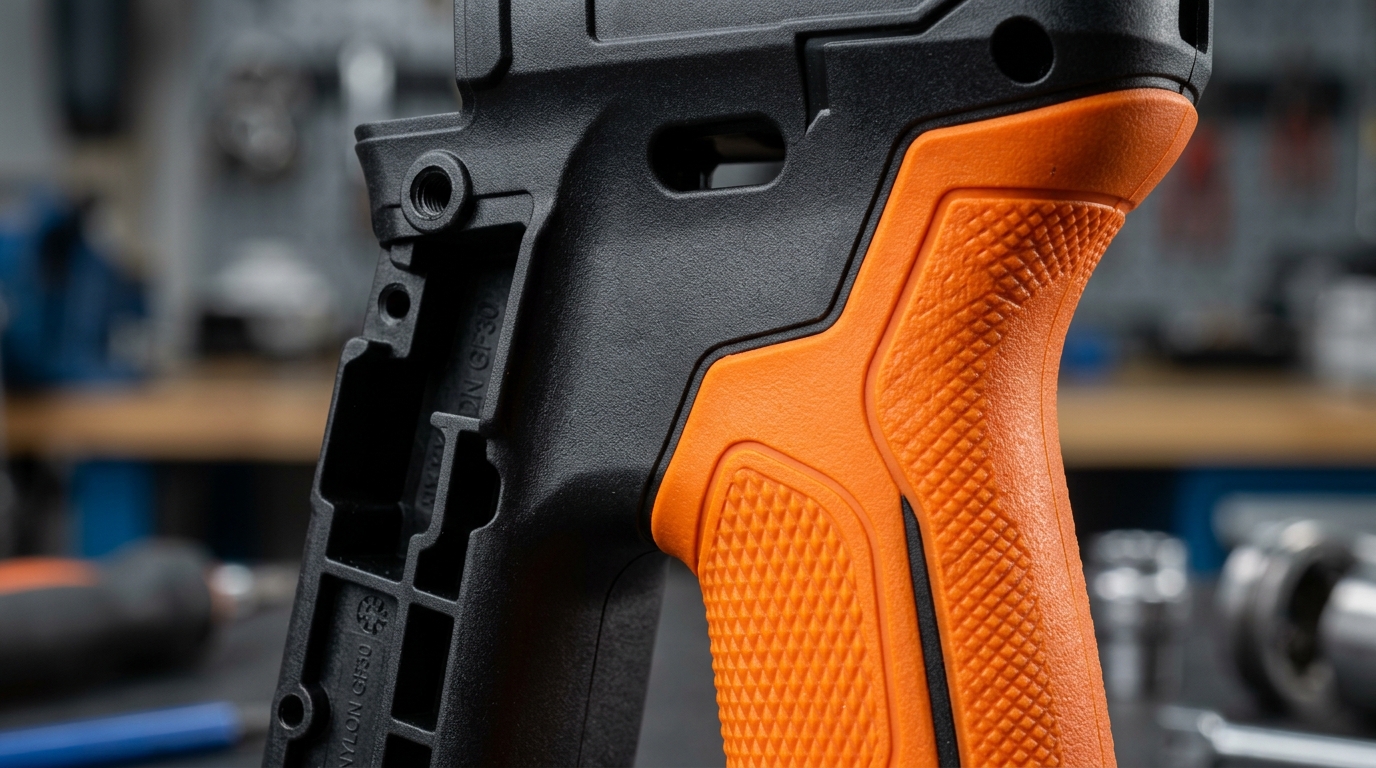
- Never use mold release spray on the primary rigid substrate.
- Dry Nylon substrates thoroughly at 100°C before second-shot molding.
- Select polarity-matched TPE grades (MAH-grafted for PA6/PA66).